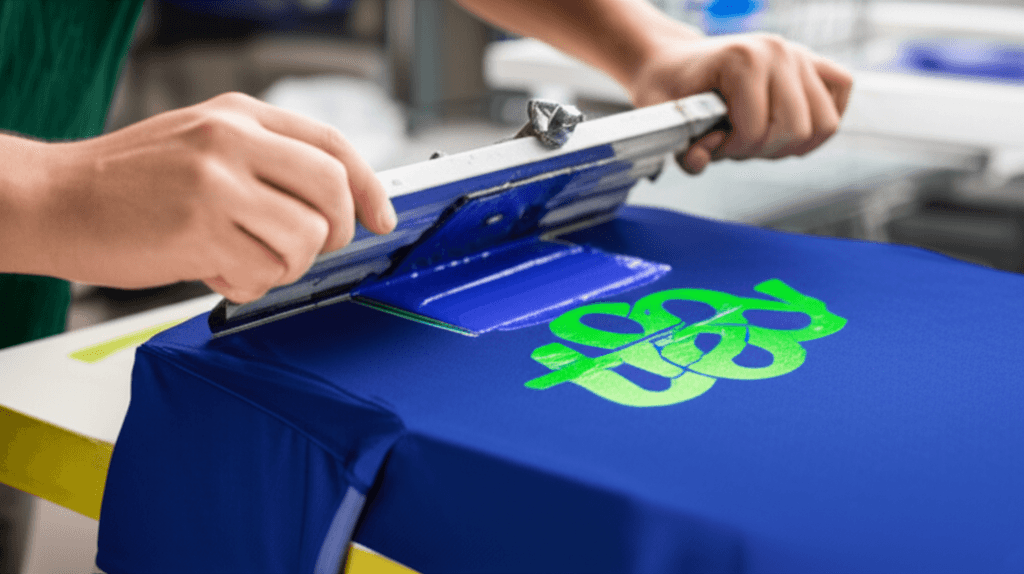
Yes, you can screen print on polyester, including performance tees, jerseys, mesh shorts and moisture-wicking polos, but it takes a different process than cotton. The garment's own dye can reactivate under heat and bleed into the ink, so polyester needs low-bleed ink, a blocker base on risky colors, lower cure temperatures and a test print. Get those right and a polyester screen print is as sharp and durable as anything on cotton.
We screen print polyester regularly at our shop at 14130 Rosecrans Ave in Santa Fe Springs, for teams, gyms and companies across Los Angeles and Orange County. Here is exactly how we keep prints from bleeding, and when we tell customers to switch to DTF instead.
What is dye migration?
Polyester is colored with disperse dyes, which bond to the fiber at high temperature. When the shirt goes through the dryer to cure the ink, that heat can turn some of the dye back into a gas. The gas moves into the ink film and shows up as color in your print.
The classic example: a white logo on a red polyester jersey looks perfect coming off the press. A few hours later, the white has gone pink. Nothing was wrong with the artwork or the screen. The jersey dye migrated into the ink, and migration can keep happening for a while after the garment cools.
It is the most common way polyester orders go wrong, and it is preventable.
Which garment colors are most likely to bleed?
| Garment color | Migration risk | What we do |
|---|---|---|
| Red, maroon, cardinal | Highest | Low-bleed ink plus gray blocker, test print first, or DTF |
| Royal, kelly green, purple | High | Low-bleed ink plus blocker, test print first |
| Orange, gold, pink | Moderate | Low-bleed ink, lowest effective cure |
| Navy, black, charcoal | Lower, but not zero | Low-bleed white underbase, test on new styles |
| White, gray, light colors | Minimal | Standard polyester process |
Heathered fabrics, dark dye lots and cheaper performance blanks vary batch to batch, so even within one brand we treat a new garment and color as untested until we have printed it.
How do you stop dye migration on polyester?
No single trick does it. These controls work together.
1. Low-bleed polyester ink
Polyester-specific plastisols, often sold as low-bleed or low-cure inks, cure at lower temperatures and contain blocking agents that resist the garment dye. White is the critical color because it shows migration first, so the white underbase and any white or light top colors go down in low-bleed ink.
2. A gray blocker base
On the worst offenders (reds, royals, greens) we print a gray blocker layer under the white. The gray traps migrating dye before it reaches the visible ink, and any slight tint it picks up is hidden under the top colors.
3. Lower cure temperatures
Cotton prints typically cure around 320 degrees F. Low-bleed polyester inks are designed to cure in roughly the 270 to 290 degree range, which means far less dye activation. We run polyester at the lowest temperature that still fully cures the ink on our gas-fired conveyor dryer and verify with temperature strips, because an undercured print will wash off no matter how good it looks.
4. Gentler flashing
Between colors, the flash unit gels the ink so the next color can print on top. On polyester we flash cooler and shorter, which protects the fabric from going shiny and avoids heating the dye more than necessary.
5. Fast cooling, no warm stacks
Migration continues while the garment is hot. Shirts come off the dryer and cool before they are stacked, because a warm stack keeps cooking the dye into the print.
6. A test print before the run
For any risky color or unfamiliar garment, we print and cure a few pieces first and let them sit before the full run goes on press. If the white holds, we run the order. If it tints, we adjust the base, switch inks or recommend DTF before you have a box of pink logos.
What other problems come up on polyester?
Adhesion. Ink sits on top of smooth synthetic fiber instead of soaking in. The fix is the right polyester ink, the right deposit (not too thin, not so thick it gets stiff) and a full cure. On blends that fight adhesion, a bonding additive in the ink helps.
Stretch. Spandex blends, compression shirts and athletic shorts stretch well past a cotton tee. Standard ink can crack when the fabric pulls. We mix a stretch additive into the ink for those garments and keep the deposit controlled. If the garment is very stretchy, DTF or stretch vinyl can be the better choice.
Moisture-wicking finishes. Some performance fabrics carry a surface treatment that resists ink. This is one more reason we test a new garment style before production.
Scorching and shine. Polyester can glaze or change texture under too much heat. Lower temperatures and short flashes keep the fabric looking like fabric.
Static and lint. Synthetics attract lint, which shows up as specks or pinholes in the print. Clean garments and a lint-free press area matter more than on cotton.
For more on why prints fail over time, see ink cracking on shirts after washing and why screen printed shirts crack.
When should you choose DTF instead?
Screen printing is the best value for simple designs at volume. DTF is the safer or cheaper call in these situations:
| Situation | Better choice |
|---|---|
| 1 to 4 color logo, 36+ pieces per design, light or mid-tone garment | Low-bleed screen print |
| Large run on a red or royal jersey that passes a test print | Low-bleed screen print with gray blocker |
| Under 36 pieces per design | DTF (starts at 12) |
| Full-color art, gradients or photos | DTF |
| Heavy spandex or compression fabric | DTF or stretch vinyl |
| Known bleeder that fails a test print | DTF |
| Individual names and numbers | Heat transfer vinyl or DTF |
DTF goes on at lower heat for a short press time and carries its own white layer, which makes it the most forgiving option on problem polyester. Compare the two methods side by side in DTF vs screen printing for polyester jerseys, or read the broader guide to printing on polyester and performance wear.
How is a polyester job priced?
Polyester runs are priced like any other screen printing order: by quantity, number of colors and print locations, plus the garment. The screen setup is built into the per-piece price, and the volume tier is based on the total pieces on the order. The minimum is 36 pieces per design. Current per-piece pricing is in the screen printing cost guide, and the quote builder prices your exact job with the garment included. If the job is a better fit for DTF, check the DTF cost guide.
How does ordering work at French Press Custom?
- Tell us the garment (brand, style and color), quantities by size, artwork and print locations.
- We confirm the right ink system for the fabric, flag risky colors, and send an estimate. Metallic inks are available at an extra charge quoted on the estimate.
- A 50% deposit starts the job, and you approve a digital proof before anything prints.
- Risky colors get a test print before the full run.
- Standard turnaround is about 2-3 weeks after the artwork is approved and the deposit is paid, and it moves with the production schedule.
- Pick up Monday through Friday, 8am to 4pm, or we ship UPS or FedEx to a street address (no PO boxes). The balance is due before pickup or shipping.
Your artwork stays on file for reorders, and a reorder of the same artwork skips the setup cost. Questions about a specific garment? Contact us with the style number and we will tell you how it prints.
Frequently asked questions
Can you screen print on 100% polyester?
Yes. 100% polyester is the most migration-prone fabric, so it gets low-bleed ink, a blocker base on risky colors, lower cure temperatures and a test print. Done that way, the print is sharp and durable.
Why did the white on my polyester shirt turn pink?
That is dye migration. The red disperse dye in the shirt reactivated under curing heat and moved into the white ink. It happens when polyester is printed with standard ink at cotton temperatures, and it is prevented with low-bleed ink, a gray blocker and lower cure heat.
What is the best ink for screen printing on polyester?
A polyester-specific low-bleed plastisol. It cures at a lower temperature and contains dye blockers, and it can be mixed with a stretch additive for spandex blends. White is the most important color to print in low-bleed ink.
Can you screen print on dri-fit or moisture-wicking shirts?
Usually, yes. Some moisture-wicking finishes resist ink, so we test print a new style before the full order. If adhesion is poor, DTF bonds reliably to treated performance fabric.
Is there a minimum for screen printing on polyester?
Yes, 36 pieces per design, the same as cotton. Under 36, DTF from 12 pieces is the usual answer on polyester, since DTG does not print well on synthetics.
Do screen prints on polyester last as long as on cotton?
Yes, when the ink is fully cured. Wash inside out in cold water, skip bleach and softener, and hang dry or tumble on low to get the longest life from any print on polyester.